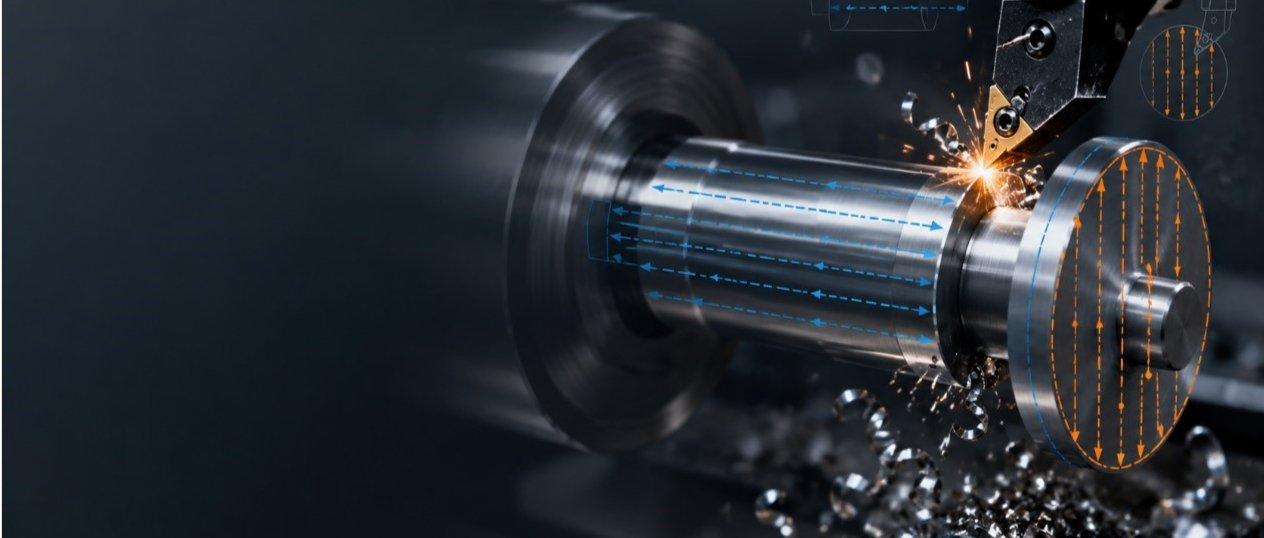
During the roughing stage of CNC turning, G71 (axial roughing cycle) and G72 (facing roughing cycle) are the two core canned cycles on a Fanuc control. New programmers may pick the wrong cycle direction, and that leads to uneven tool loading, poor chip evacuation, or an alarm when the part's profile has a groove.
Picking the right cycle and dialing in the parameters correctly can cut your cycle time by a real margin. This article breaks down the difference between these two cycles, the correct syntax, and a few practical tips for optimizing your toolpath.
G71 vs. G72: Cutting Direction Decides Part Quality
Do not start by asking "how do I want to cut this?" Start with the shape of the part and its rigidity requirements.
| Criteria |
G71 (axial roughing cycle) |
G72 (facing roughing cycle) |
| Cutting direction |
Moves back and forth mainly along the Z axis (axial) |
Moves back and forth mainly along the X axis (radial) |
| Best suited for | Shaft-type parts and tubing with a large length-to-diameter ratio | Disc-type parts, flanges, and gear blanks with a large diameter |
| Cutting force | Higher side load — best for parts supported by a tailstock | Higher axial thrust — best for parts with strong chuck-face support |
| Chip evacuation | Good for long OD cuts, though the chip path is longer | Good for large face work — centrifugal force helps clear chips |
Program Format (Fanuc Two-Block Command)
1. G71 Axial Roughing Format
G71 U(d) R(e) ;
G71 P(ns) Q(nf) U(u) W(w) F(f) ;
- Block 1, U(d): Depth of cut per pass (given as a radius value).
- Block 1, R(e): Retract amount.
- Block 2, P(ns): Sequence number of the first block in the finishing contour program.
- Block 2, Q(nf): Sequence number of the last block in the finishing contour program.
- Block 2, U(u): X-axis finishing allowance (given as a diameter value).
- Block 2, W(w): Z-axis finishing allowance.
- Block 2, F(f): Feedrate for the roughing cut.
2. G72 Facing Roughing Format
G72 W(d) R(e) ;
G72 P(ns) Q(nf) U(u) W(w) F(f) ;
- Block 1, W(d): Depth of cut per pass along the Z direction.
- Block 1, R(e): Retract amount.
- Block 2, P(ns): Sequence number of the first block in the finishing contour program.
- Block 2, Q(nf): Sequence number of the last block in the finishing contour program.
- Block 2, U(u): X-axis finishing allowance (given as a diameter value).
- Block 2, W(w): Z-axis finishing allowance.
- Block 2, F(f): Feedrate for the roughing cut.
The Key Difference Between Type I and Type II
This is a detail a lot of programmers overlook, and it decides whether the machine can cut a contour with a groove in it.
Type I (Monotonic Contour).
- Definition: The contour can only increase or decrease in one direction along the X axis or the Z axis. It cannot double back on itself — in other words, no grooves.
- How to call it: In the block marked by the sequence number under P (for example, N100), write only the X-axis coordinate.
Type II (Non-Monotonic Contour).
- Definition: The contour is allowed to have a recessed section or a pocket. The control automatically detects the recess and cuts it in multiple steps.
- How to call it: In the block marked by the sequence number under P (for example, N100), write both the X-axis and Z-axis coordinates — even if the Z movement is zero, you still have to write Z0. This is useful on Focus CNC machines when you are cutting a complex pulley or sheave profile.
Practical Optimization Tips
1. The Starting Point Matters.
Before you run G71 or G72, where you position the tool before the cycle starts is critical. The starting point has to sit outside the raw stock diameter. For G72 facing, if you leave too little clearance on the Z axis and the raw stock face is not flat, the first pass can take an excessively deep cut and chip or break the insert. As a general rule, leave at least 2 to 5 mm of clearance on the Z axis.
2. Pay Attention to the Sign of U and W.
The sign of the finishing allowance values U and W determines which direction the allowance is applied.
- OD machining: U and W are usually positive.
- Bore machining: U is usually negative, since the allowance is left on the inside of the bore.
3. Pair G70 with the Same Block Range to Avoid Air Cutting.
Once roughing is done, call G70 P100 Q200 to reference the same contour for the finish cut. This keeps your program simple, and it also ensures the roughing and finishing toolpaths follow the exact same line.
Getting Better Results from G71 and G72 Roughing Cycles
The choice between G71 and G72 ultimately depends on the part geometry and the direction in which material needs to be removed. G71 is generally suited to axial roughing on shaft-type parts, while G72 is better suited to facing operations on larger-diameter parts. Beyond choosing the cycle itself, setting the correct starting point, finishing allowances, and contour type can help create a more efficient and predictable roughing process.
For manufacturers evaluating CNC turning equipment for specific part geometries or machining requirements, contact Focus CNC to discuss your application and explore suitable CNC lathe options.